


Industrial-Grade
Floor Coatings
Built for Southern Utah’s Toughest Environments
Heavy machinery. Metal fabrication. Chemical exposure. When your operation can’t afford coating failure, you need three decades of proven industrial performance to get the job done right.

When Standard Coatings Fail, Industries Pay the Price
Standard residential-grade coatings weren’t designed for the punishment your facility dishes out. And when they fail, you pay in ways that go far beyond the initial coating cost.
The Hidden Costs of Coating Failure:
- Unplanned downtime while emergency repairs shut down production lines
- Safety hazards from damaged, uneven, or chemically compromised surfaces
- Frequent recoating cycles that disrupt operations every few years
- Equipment damage from debris, dust, and unstable flooring
- Regulatory compliance issues in food processing, pharmaceutical, or safety-critical environments
Hi Tech Coatings eliminates these problems with industrial systems engineered for your specific operational demands. In 30 years of serving Southern Utah’s industrial sector, we’ve never had a single coating failure—because we understand that in industrial environments, “good enough” isn’t good enough.
Our Expertise:
Three Decades of Industrial Excellence
Since 1994, Hi Tech Coatings has been the trusted partner for Southern Utah’s most demanding industrial facilities.
From St. George manufacturing plants to Cedar City fabrication shops, we’ve protected floors that endure punishment most coatings can’t survive.
Our Premium Military-Grade Industrial Systems
Our most advanced coating solution isn’t just built for heavy traffic—it’s engineered for environments where engines are rebuilt, tanks are fabricated, and heavy metal components are regularly moved or dropped.
Tier 3 “Industrial Fortress” – Our Premium Military-Grade System
- Specialized chemical formulations that bond at the molecular level with properly prepared concrete
- Extreme impact resistance tested against dropped steel plates and heavy machinery loads
- Chemical barrier protection against oils, solvents, acids, and industrial cleaning agents
- Temperature stability that performs in Southern Utah’s extreme heat and rapid temperature changes
Specialized Military-Industrial Applications:
- Commercial Dustproofing Systems – Eliminate concrete dust in manufacturing and warehouse environments
- Food-Grade Systems – FDA-compliant coatings for processing facilities and commercial kitchens
- Epoxy/Polyurethane Hybrid Systems – Maximum chemical resistance for extreme industrial environments
- Quartz Crystal Systems – Ultimate durability with enhanced slip resistance and impact protection
- Polished Concrete Solutions – High-performance, low-maintenance floors for manufacturing facilities
Industries We Serve
Specialized Solutions for Every Industrial Environment
Aircraft Hangars
Fuel spills, hydraulic fluids, and heavy aircraft loads require military-grade coatings with exceptional chemical resistance and load-bearing capacity. Our specialized systems handle jet fuel, de-icing fluids, and extreme temperature variations.

Manufacturing Facilities
Heavy machinery operations, assembly lines, and production floors demand chemical resistance and extreme durability. Our commercial dustproofing systems eliminate concrete dust while providing the impact resistance manufacturing requires.
Warehouses & Distribution Centers
High-traffic forklift operations, pallet drops, and 24/7 logistics operations require coatings that never quit. Our polished concrete solutions provide low-maintenance, high-performance floors that withstand constant use.


Automotive Service Centers
Oil spills, brake fluid, transmission fluid, and heavy lift equipment demand our specialized epoxy/polyurethane hybrid systems with maximum chemical resistance and easy cleanup.
Commercial Kitchens
Food service environments require our FDA-compliant food-grade systems that resist cleaning chemicals, maintain sanitary conditions, and meet strict health department regulations.

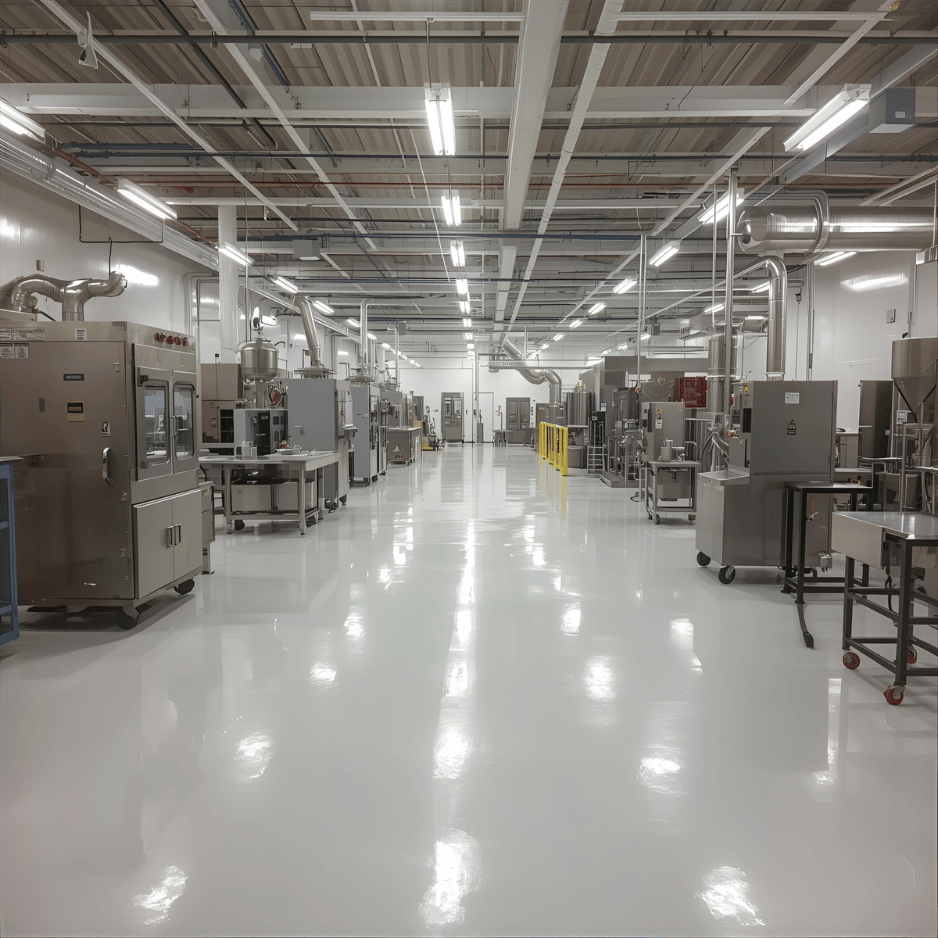
Food Processing & Manufacturing Plants
Strict regulatory compliance, chemical washdown compatibility, and sanitary requirements demand our specialized food-grade systems engineered for processing environments with enhanced slip resistance and bacteria-resistant properties.
Our Industrial Process
Engineered for Minimal Disruption, Maximum Performance
Phase 1
Specialized Surface Preparation
Industrial environments require aggressive surface prep that goes far beyond residential standards. Our diamond grinding and shot-blasting techniques create the mechanical bond profile necessary for permanent adhesion under extreme conditions.


Phase 2
Military-Grade System Selection
Every industrial facility is different. We analyze your specific operational requirements—chemical exposures, load patterns, temperature ranges, and regulatory compliance—to select the optimal military-grade system:
- Military-Grade Industrial Fortress for extreme heavy-duty applications
- Commercial Dustproofing Systems for manufacturing environments requiring dust elimination
- Food-Grade Systems for processing facilities and commercial kitchens
- Epoxy/Polyurethane Hybrids for maximum chemical resistance
- Quartz Crystal Systems for ultimate impact resistance and slip protection
- Polished Concrete for low-maintenance, high-performance manufacturing floors
Phase 3
Minimal Downtime Installation
We understand that every hour of downtime costs money. Our industrial installation teams work with your production schedule to minimize operational disruption, often completing sections during planned maintenance windows.


Phase 4
Post-Installation Testing & Validation
Before we consider the job complete, we conduct adhesion testing, chemical resistance verification, and load testing to ensure your new floor system meets or exceeds specifications.
Featured Project:
Randolph Air Force Base – San Antonio, TX
Challenge: Historic 1930s aircraft hangar requiring complete floor restoration while maintaining operational readiness. 25,000 square feet of aging concrete needed military-specification coating capable of supporting modern aircraft operations and fuel/chemical exposure.
Solution: Full Industrial Fortress military-grade system with specialized surface preparation for historic concrete.
Project Scale:
- Team of 11 specialists for comprehensive surface preparation (3 days)
- Team of 7 for precision installation
- 7 total days with military-precision timing
- Decades of aviation history restored for continued service

Results: Successfully delivered military-specification performance on schedule, restored structural integrity of historic facility, provided long-term protection for continued military operations.
The Track Record That Matters
Why Industries Choose Hi Tech Coatings

30 Years of Experience
In three decades of industrial projects, we’ve built our reputation on solutions that endure. Our track record speaks for itself. When industries choose Hi Tech Coatings, they’re choosing proven expertise and long-term reliability.

Contractor-Trusted Expertise
Southern Utah’s industrial contractors rely on our technical guidance for their most challenging projects. When construction professionals trust us with their reputation, you know you’re working with proven experts.

Deep Understanding of Industrial Operational Demands
We don’t just apply coatings—we solve industrial flooring problems. Our team understands production schedules, safety requirements, regulatory compliance, and the true cost of operational disruption.
Industrial Services Across the Western United States
Primary Service Areas
We frequently serve industrial facilities throughout Arizona, Idaho, Utah, and Nevada with comprehensive project management and local support.
Extended Project Capabilities
For large-scale industrial projects like our recent Randolph Air Force Base installation, we bring our military-grade expertise to facilities across the United States.
Our team is equipped to handle significant industrial projects regardless of location when the scope and requirements align with our specialized capabilities.

Get Started with Your Industrial Floor Solution
Professional Industrial Consultation Process
Ready to eliminate floor coating problems permanently? Our industrial consultation process ensures you get the right solution for your specific operational requirements.
Step 1: Facility Assessment
Our industrial specialists conduct a valuation of your operational requirements, existing floor conditions, chemical exposures, and performance expectations.
Step 2: Custom System Design
Based on your facility’s unique demands, we engineer a coating system specifically designed for your operational environment and budget requirements.
Step 3: Installation Planning
We work with your production schedule to minimize operational disruption, often coordinating with planned maintenance windows or facility downtime.
Step 4: Professional Installation
Our certified industrial installation teams deliver the performance you need with the reliability you expect from 30 years of proven expertise.
Step 5: Quality Inspection & Warranty
Every installation is thoroughly inspected to meet our high standards, backed by our company’s mission, comprehensive warranty.
Contact Our Industrial Team Today
Don’t settle for a cracked, stained concrete garage floor when you could have a beautiful, durable coating system that lasts decades. Hi Tech Coatings makes industrial coatings easy and up to par with the quality you need.